Buyer article
How Continuous Filling Changes a Tomato Sauce Bottling Line
Continuous filling changes the bottling line by moving dosing into the conveyor flow instead of treating filling as a separate stop-and-start operation. For tomato sauce, paste, ketchup, and related high-viscosity products, the key is coordinated integration from filling through downstream packaging.
The decision this page helps you make
The main change is process coordination: following filling keeps dosing inside the conveyor flow, while downstream modules can be connected around the same line logic. The project should be evaluated as a complete filling and packaging workflow, not as an isolated filler.
Buyer questions answered here
Why can stopping bottles disrupt a tomato sauce bottling rhythm? The brief identifies stop-and-start filling as a source of waiting and unstable line continuity. Continuous conveyor filling addresses that process gap by performing the filling action while containers move.
What is the role of following filling? BOJLINE uses a following-filling concept in which the filling heads move with the conveyed containers during dosing, so the line does not need to treat filling as a separate stop point.
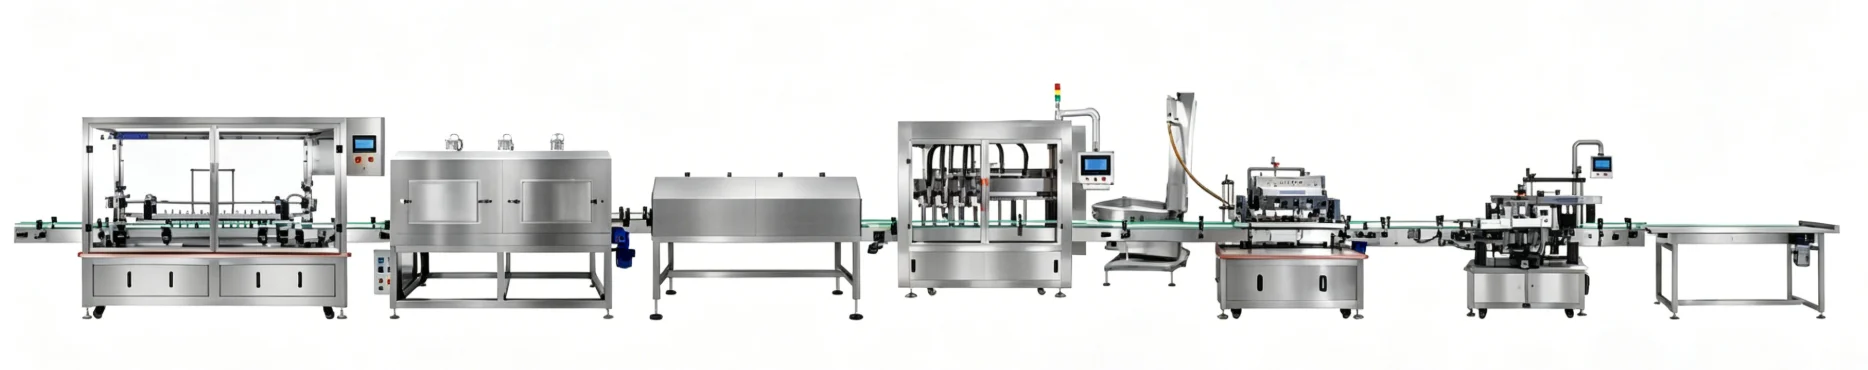
Which operations can be connected after filling? The documented chain includes capping, checkweighing, date and batch coding, labeling, shrink sleeving, and collection. Depending on the project, bottle handling, washing, and drying can also be part of the connected workflow.
How are hygiene and traceability addressed? The documented functions include CIP in-place cleaning, steam vacuum capping, CO2 laser coding, metal detection, and checkweighing. These are process functions to evaluate for the food line, not a substitute for project-specific validation.
Why stop-and-start filling creates a rhythm problem
In a conventional stop-and-start arrangement, containers wait at the filling point before dosing can begin. For tomato sauce, tomato paste, ketchup, and other high-viscosity products, that waiting point separates filling from the rest of the conveyor process and makes line continuity a central engineering question.
The practical issue is not only the filler itself. When filling, capping, inspection, coding, and labeling are treated as separate islands, each handoff can introduce waiting or interrupt the intended flow. A continuous line therefore starts with the relationship between the filling action and the conveyor rhythm.
Following filling moves dosing into the conveyor flow
The BOJLINE brief defines a two-head following-filling concept: the filling action follows the conveyed containers instead of requiring them to stop for every dose. This changes the design logic from a stop point to a coordinated moving operation.
For a factory team, the benefit to examine is the change in handoff logic: containers remain part of the conveyor flow while dosing takes place, and the next packaging operations can be planned around that flow. This explains why continuous filling is a line-level decision rather than a single-machine feature.
From filling to a connected packaging chain
The documented BOJLINE workflow can connect bottle handling, washing, drying, filling, capping, checkweighing, coding, labeling, shrink sleeving, and collection. The exact combination depends on the factory project, but the operating idea is consistent: connect the handoffs instead of leaving each operation as a separate manual island.
This structure is relevant to tomato sauce bottling lines, tomato paste filling lines, ketchup packaging lines, and tomato diced-product replenishment lines. It also gives production and procurement teams a clearer way to compare a standalone filler with a complete filling and packaging solution.
Hygiene, inspection, and traceability remain part of the rhythm
A faster-looking conveyor layout is not enough for a food factory. The documented line functions include CIP in-place cleaning, steam vacuum capping, CO2 laser coding for dates and batches, metal detection, and checkweighing for quality control. These functions connect production rhythm with hygiene and release checks.
For engineering, production, and procurement teams, the next step is to define the material, container format, existing operations, and required downstream modules before discussing a line configuration. The available source material does not confirm numeric capacity, speed, dosing accuracy, volume range, or container range, so those items require project-specific validation.
Planning a Tomato Sauce Bottling Upgrade?
Share your product, container format, existing operations, and required downstream modules with the project team for a process-level discussion.