Buyer article
Why the bottle cannot stop during tomato sauce filling: how BOJLINE changes the line rhythm
For manufacturers of ketchup, tomato paste, and tomato sauce: how BOJLINE connects continuous infeed, filling of viscous products, and downstream packaging without unnecessary stops.
The decision this page helps you make
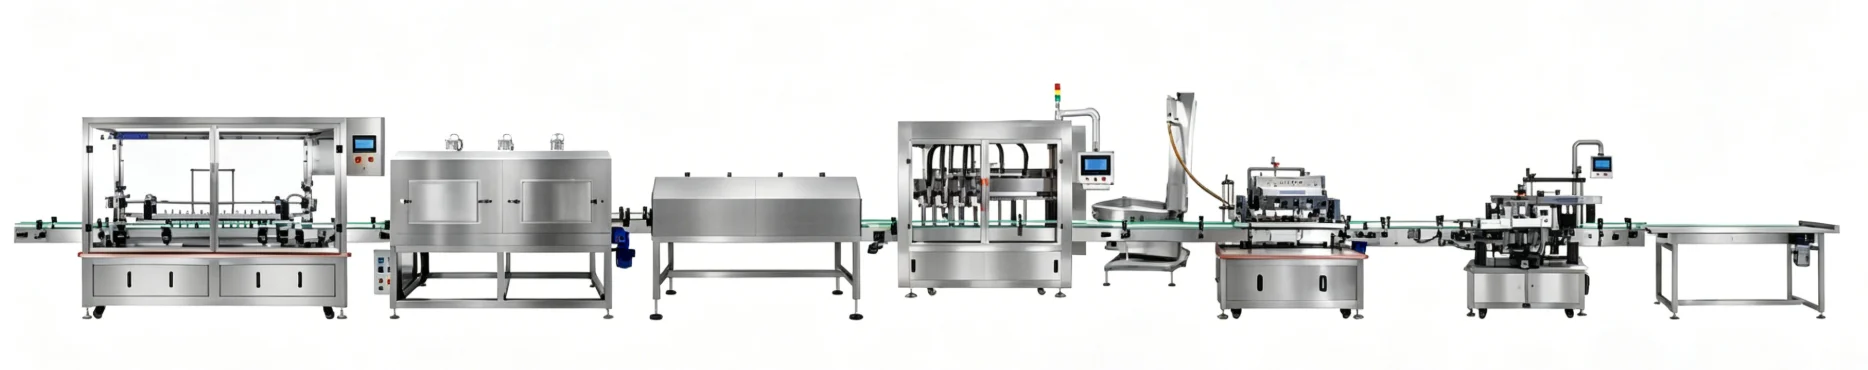
When a plant moves from manual or semi-automatic filling to an automatic ketchup packaging line, the key question concerns more than the dispenser itself. BOJLINE builds a continuous sequence: container infeed, filling of viscous products while containers are moving, capping, inspection, coding, and labeling.
Buyer questions answered here
Why does stopping the bottle disrupt the rhythm of a tomato sauce filling line? In a manual or semi-automatic setup, stopping the bottle before filling interrupts the flow: an operator or separate machine has to repeat the positioning, while downstream operations do not receive containers at a consistent rate.
Why does high-viscosity tomato production require a coordinated line? For ketchup, tomato paste, tomato sauce, and tomato products with particulates, coordinated hopper infeed, container movement, and filling-unit operation are important; therefore, filling, capping, and subsequent inspections should be considered as one connected line.
What changes after downstream modules are connected? Instead of separate operations, the plant gains a sequence that includes cap placement or tightening, checkweighing, date and batch coding, labeling, and collection of finished containers; the specific configuration is determined by the line project.
Who needs continuous tomato sauce filling
This topic is especially relevant to plants producing ketchup, tomato paste, tomato sauce, and tomato products with particulates. Such a sauce packaging line is also needed by companies modernizing an existing section where bottles or jars move between separate manual and semi-automatic operations.
In projects of this kind, the task is not simply to add an automatic sauce dispenser. The container infeed, filling, closing, and inspection must be coordinated so that each downstream operation receives the product within the overall flow rather than after another pause.
What happens when the bottle has to stop
With manual or semi-automatic filling, the bottle often has to stop beneath the filling unit. It then needs to be returned to the flow, passed to the next operator or machine, and held until the next position is ready. This setup creates gaps between operations and makes it more difficult to maintain a consistent line rhythm.
The problem is more noticeable with viscous products: tomato sauce and tomato paste require coordinated infeed and dosing rather than filling whenever a workstation becomes available. Therefore, a viscous-product filling line should be designed around container movement and a stable sequence of operations, without adding unverified speed or output figures.
How BOJLINE fills while containers are moving
BOJLINE is based on a dual-head tracking system: filling takes place while containers move along the conveyor, so the bottle does not need to stop before filling. The hopper feeds product to the filling unit, while the guides help align the container with the working zone.
This approach is suitable for a tomato sauce filling line, a ketchup packaging line, and other sections where continuous infeed, hygienic design, and the ability to connect the main unit with downstream packaging are important. BOJLINE materials do not specify universal output, accuracy, volume, or container-range values, so these parameters must be determined separately for each project.
From the filling head to coding: one continuous flow of operations
Continuous filling reveals the value of an integrated line only when the downstream section does not return containers to manual processing. Depending on the project, the sequence may include container orientation and infeed, washing and drying, filling, cap tightening, checkweighing, date and batch coding, labeling, shrink-sleeve labeling, and collection of finished products.
For end-of-line inspection, the solution may include metal detection and weight-based sorting. Clean-in-place, or CIP, supports the line's sanitation logic, while CO2 laser marking helps apply the date and batch number. These are not separate promises of results but functional modules provided for and selected according to the food plant's requirements.
Connecting the conveyor, filling heads, hopper, capping section, checkweigher, coder, and labeler shifts the discussion from a single machine to the level of the entire filling and packaging line.
What a food plant gains by switching to a continuous line
For a plant, switching to BOJLINE means changing the logic of the section: instead of separate stops and manual transfers, it creates a sequential route from container infeed to packaging. This helps frame the tomato sauce filling line as one modernization project rather than a set of disconnected machines.
The final configuration can be built around bottled or canned products and supplemented with the required inspection, coding, and labeling operations. At the same time, the equipment configuration, container characteristics, and operating parameters must be confirmed during the design stage; BOJLINE should not be described using unverified figures, certificates, or promises of a specific result.
Discuss modernization of a tomato sauce packaging line
Describe the current section, the type of tomato product, and the operations required after filling. Specialists can discuss the configuration of a continuous line, including infeed, filling, capping, inspection, coding, and labeling.