Buyer article
Where to Adjust First When Changing Bottle Formats on a Sauce Filling Machine
When a food factory changes bottle formats, start with the container path and alignment—not with unsupported assumptions about speed or changeover time. This checklist follows the adjustable parts documented for FTPfill: clamps, guides, filling-head height, replaceable nozzles, tracking motion, product lines, and HMI settings.
The decision this page helps you make
For a new bottle format, begin with stable container handling and the bottle centerline: adjust the clamp spacing and guide plates, then check filling-head height and nozzle alignment. Only after the mechanical path is matched should the team review tracking motion, product-path connections, and HMI settings. FTPfill documentation confirms these adjustment points, but does not provide a universal changeover time, filling speed, accuracy, size, or viscosity limit.
Buyer questions answered here
What should be adjusted first when changing a bottle format? Start with the container path: the clamp spacing and adjustable guide plates keep the bottle aligned before the filling-head position is checked.
How does the filling head fit a different bottle? The filling heads can move vertically, the clamp spacing and guides are adjustable, and the filling nozzles are replaceable according to the documented product materials. The exact setting depends on the actual bottle and must be confirmed during application assessment.
Does the available material specify a universal changeover time or filling performance? No. The FTPfill materials do not provide changeover time, filling speed, filling range, accuracy, machine dimensions, or an upper viscosity limit, so these figures should not be assumed for a new format.
1. Start with the container path, not the recipe on the HMI
A bottle-format change affects the relationship between the conveyor, the bottle body, the neck, and the filling nozzle. FTPfill documentation identifies different bottle necks, heights, or diameters as reasons to readjust the clamps and guide plates; without that alignment, the nozzle may not remain stably over the opening.
The first engineering question is therefore: can the new container travel along the existing chain conveyor while remaining centered and controlled? Check the clamp spacing, adjustable guide plates, and the bottle path before treating HMI values as the main changeover task.
2. Check clamps and guides for stable neck-to-nozzle alignment
Use the new bottle’s actual neck and body dimensions as the reference for the mechanical adjustment. The documented FTPfill structure includes adjustable clamp spacing and guide plates. These are the first physical points to inspect because they control how the bottle is presented to the filling heads.
A useful handoff note for engineering and purchasing is not simply “new bottle accepted.” Record which container features need adjustment: neck position, bottle height, body diameter, clamp spacing, guide position, and whether the existing nozzle arrangement can stay aligned. The materials confirm the adjustment functions, but do not provide a universal compatibility table.
3. Then check filling-head height, nozzle choice, and tracking motion
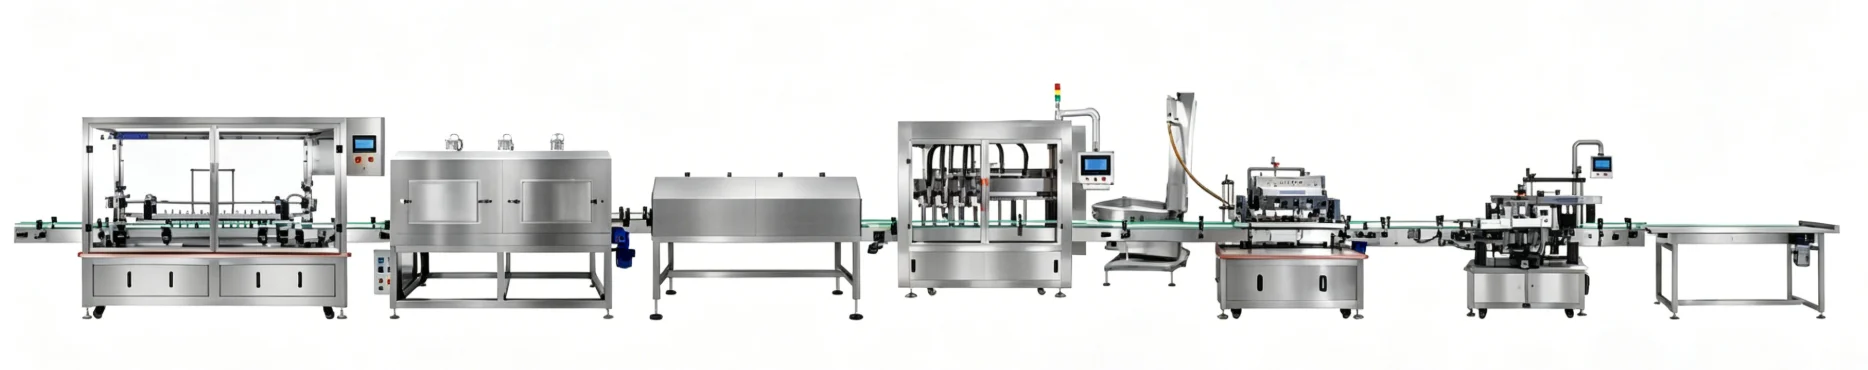
FTPfill uses a tracking filling arrangement: the chain conveyor moves the container forward while the filling heads move in the same direction and follow the container. The filling heads can move vertically, and the materials state that the nozzles can be replaced. For a new format, check vertical clearance, nozzle-to-opening alignment, and whether the head movement follows the container path without forcing the bottle to stop.
This is also where the process boundary matters. Dynamic tracking is documented as a way to avoid repeated container stop-and-start, which can make thick products splash or become unstable. It does not by itself prove a particular speed, filling accuracy, or suitability for every sauce; those values are not supplied and require application confirmation.
4. Finish with product path, cleaning access, and HMI settings
After the bottle path and filling-head position are reviewed, inspect the product-contact side: the hopper level sensor, material pipes, three-way rotary valve, filling valves, cleaning lines, and quick-release connections. These components are part of the documented FTPfill structure for feeding, metering, filling, and cleaning access; the materials do not define a validated CIP cycle or cleaning parameters.
The HMI is the final control-point review, not the first substitute for mechanical alignment. The documented interface can set filling volume and filling speed and show running status and production data. Review those settings only after the new container path and head position have been checked, and do not convert the presence of a setting into a guaranteed performance figure.
Need to assess a new bottle format?
Send the bottle format, sauce or thick-food material details, and the intended line arrangement to the CODAPAK team for an application review focused on container alignment, filling-head adjustment, and product-path requirements.