Buyer article
Four-head piston machine with tracking: checklist before a format changeover for sauce filling
A practical checklist for engineering, production, and procurement teams: what to check in the container, positioning zone, dosing circuit, controls, and FTPfill cleaning before a format changeover on a viscous product filling line.
The decision this page helps you make
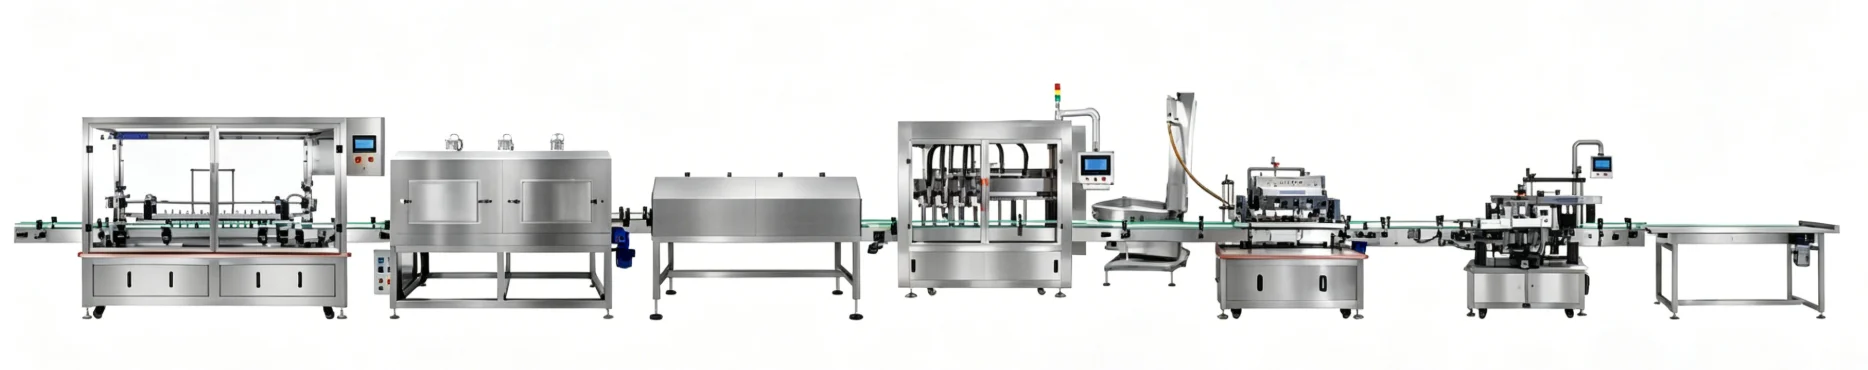
Before requesting sauce filling equipment, record the container type, bottle or can characteristics, product, and expected sequence of operations. Then check the relative positions of the conveyor, guides, clamps, and filling heads, as well as access to the piping and HMI settings. This sequence helps enable a specific discussion of the FTPfill configuration without replacing verification with performance promises.
Buyer questions answered here
Why is tracking used when filling thick sauces instead of stop-and-fill only? With tracking filling, the container continues moving while the heads move synchronously with it, so repeated stopping and starting of the container associated with product surging and splashing is not required.
What should be checked first when changing a bottle or can? Confirm the container type and check that its height, diameter, and neck match the line settings; then inspect the adjustable guides, distance between clamps, head height, and condition of the filling nozzles.
What is included in the FTPfill dosing circuit? Four piston dosing units perform product suction, dosing, and delivery; the circuit also includes piping, a three-way rotary valve, filling valves, and quick-release connections.
Can this checklist be used to state the changeover time or accuracy? No. The materials contain no confirmed values for format-changeover time, speed, volume range, or error, so these must be agreed separately for the specific product and container.
1. Record the container and product before setup
Start by recording what is changing: bottle or can, glass or PET container, and the height, diameter, and shape of the neck. Record the product separately—for example, ketchup, tomato paste, or another thick sauce—because the dosing-unit configuration for viscous products must be discussed together with the characteristics of the specific material.
Do not replace this check with a general inquiry about ketchup filling equipment. For engineering discussions, the actual containers, product, and product delivery scheme to the machine are important.
2. Check container infeed and the positioning point
Make sure the chain conveyor feeds the containers along a stable path and that the adjustable guides hold them in the working zone. Check the distance between the clamps for bottles and the position of the neck relative to the filling nozzles.
Before the trial cycle, also check the head height: on FTPfill, their vertical movement is controlled by a cylinder, and their position must correspond to the specific container. If required, the nozzles can be replaced; this should be confirmed before starting the setup.
3. Inspect the piston filler and product circuit
Check the four piston units as one sequence: product suction, dosing, and delivery into the container. The FTPfill materials state that each piston pump is servo-driven, while speed and number of revolutions are used to control the piston stroke.
Inspect the three-way rotary valve, filling valves, sanitary piping, and quick-release connections. For thick sauces, access to these components is important when checking the dosing circuit and subsequent cleaning.
4. Check tracking movement and HMI settings
Check that the heads can move horizontally following the container, rather than only performing positional filling. The four filling heads synchronize with the movement of the containers along the chain conveyor; this is the key feature of FTPfill sauce-filling equipment.
On the HMI, check the availability of volume and speed settings, the display of operating status, and data on the number of containers filled. Do not record numerical values without separate agreement: the available materials confirm the interface functions, but not specified throughput or dosing range.
5. Complete the check with cleaning and safe observation
Before completing the format changeover, check access to the dismantlable sections of the product line, quick-release connections, the flushing pipeline, and the wastewater collection tank. Make sure the cleaning procedure is clear to the operator and does not require attributing unconfirmed CIP modes to the machine.
Finally, inspect the transparent tempered safety door and the ability to observe the units without opening the guard. Then separately agree with the engineering team on a trial run using the actual container and product; the changeover time and test result are not stated in advance.
Do you need to check the configuration for your container and sauce?
Provide information about the product, container, and existing line. The team can discuss the positioning, dosing, cleaning, and control points that should be confirmed before the format changeover.