Buyer article
BOJLINE: how filling in motion changes bottle-line rhythm
Understand filling during conveying and how feeding, downstream operations and cleaning controls affect line rhythm.
The decision this page helps you make
Understand filling during conveying and how feeding, downstream operations and cleaning controls affect line rhythm.
Buyer questions answered here
Why can continuous filling change the line rhythm? Because filling is performed during conveying rather than after each container stops, reducing the waiting step described in the brief.
Which tomato products are in scope? The current materials name tomato sauce, tomato paste, ketchup, and tomato products with added juice around diced tomatoes, all within the high-viscosity tomato line context.
What operations can follow filling? The documented process chain includes capping, checkweighing, date and batch coding, labeling, sleeve shrinking, and collection, with other upstream or downstream modules selected for the project.
How is food-line control addressed? The materials identify CIP in-place cleaning, food-oriented design, metal detection, checkweighing, and CO2 laser coding as relevant functions for hygiene and traceability.
From Stop-and-Fill to Fill-in-Conveying
A stop-and-fill sequence inserts a waiting point before each filling action. The BOJLINE brief describes another operating logic: filling takes place while containers are being conveyed, so the line does not depend on a separate stop for every container. The practical focus is not an unverified speed claim; it is the removal of a repeated waiting step from the process logic.
This approach is positioned for viscous tomato products such as tomato sauce, tomato paste, ketchup, and tomato products with added juice around diced tomatoes. The same product context also identifies continuous filling and portioning as the core use, keeping the discussion within the tomato-processing line rather than extending it to unrelated industries.
The Line Rhythm Is Built Across Connected Operations
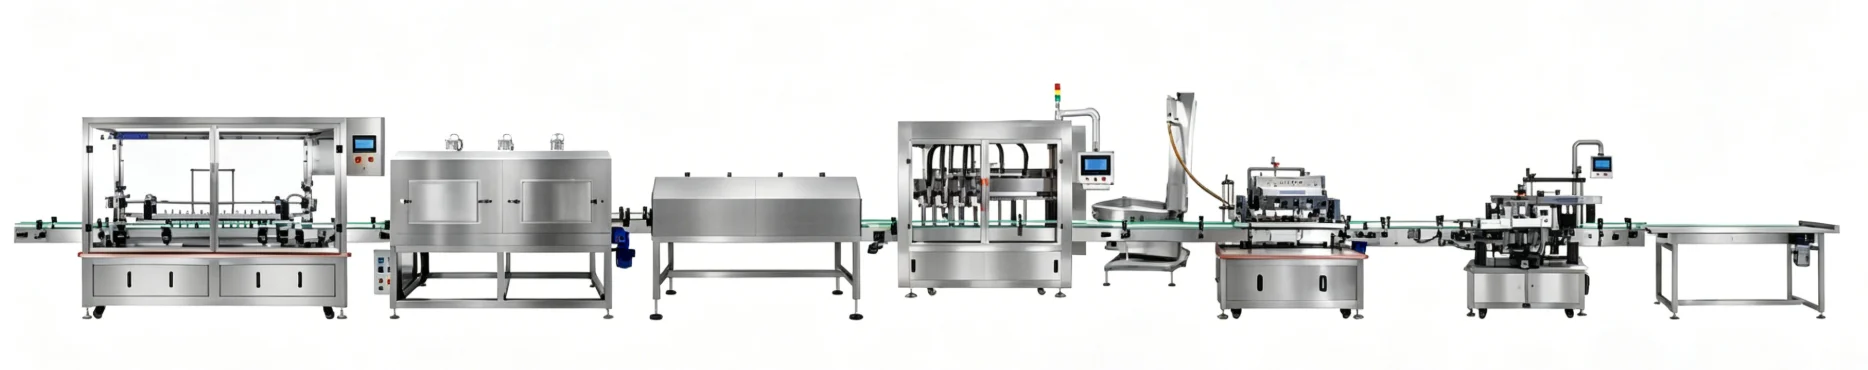
Continuous filling has more value when it is connected to the operations around it. The documented chain runs from bottle handling, washing, and drying to filling, capping, checkweighing, coding, labeling, sleeve shrinking, and collection. This turns the filling station from an isolated machine into one controlled section of a packaging line.
For a factory project, the relevant question is therefore not only whether a filler can handle a viscous product. It is also how the filler interfaces with container movement, capping, quality checks, coding, labeling, and collection. BOJLINE is presented as a modular line concept for bottle or jar packaging and for linking these stages according to the project.
A More Useful Rhythm Also Needs Hygiene and Control
A continuous line still has to meet food-factory requirements. The current materials identify in-place CIP cleaning and food-oriented design as part of the hygiene approach. They also list metal detection and checkweighing for end-of-line quality control, while CO2 laser coding supports date and batch identification.
This is why a line-rhythm discussion should include more than the filling motion itself. The project must define how cleaning, product handling, inspection, coding, and packaging work together. The materials describe these as selectable or connectable line functions, but they do not provide numeric performance, container ranges, or a universal configuration.
Evaluate the Next Bottling-Line Step
Share your tomato product, container format, and current line layout to discuss a suitable filling and packaging configuration.