Buyer article
Why Tomato Sauce Filling Should Not Stop the Bottle: How Continuous Filling Changes Line Rhythm
For tomato sauce, paste, ketchup, and other viscous foods, filling during conveying can keep the line moving instead of making every container wait at the filling point. This article explains the production logic and the modules a factory team should evaluate.
The decision this page helps you make
A continuous tomato sauce line changes the evaluation focus: instead of viewing the filler as an isolated machine, the project team should assess the conveying-and-filling logic together with capping, checkweighing, coding, labeling, hygiene, and end-of-line rejection.
Buyer questions answered here
Why is stopping the bottle a problem for a tomato sauce line? A stop-and-fill sequence inserts waiting into the conveying rhythm. BOJLINE uses two-head tracking filling so filling can take place while containers move through the line, reducing stop-and-wait logic at the filling station.
What products is the line intended for? The verified product context covers tomato sauce, tomato paste, ketchup, tomato products with replenishing juice, and other viscous tomato-food applications, with bottle and jar line integration as a project direction.
Which downstream modules can be linked after filling? The documented process chain includes capping, checkweighing, date and batch coding, labeling, sleeve shrinking, and collection. Bottle handling may also be arranged through bottle sorting, washing, and drying before filling.
How should a factory evaluate hygiene and quality-control functions? The available materials identify CIP in-place cleaning, a steam vacuum capping function, food-grade design, CO₂ laser coding, metal detection, and checkweighing as relevant line functions. Their final configuration should be confirmed against the project requirements.
The key change: filling follows the moving container
In a stop-and-fill arrangement, the container must wait for the filling action to finish before it can continue. For viscous tomato sauce, tomato paste, and ketchup, that waiting point becomes part of the line rhythm. BOJLINE is positioned around a different logic: two-head tracking filling completes the filling action while the container is conveyed, so the line does not depend on stopping every bottle at the filler.
This is not a claim about a specific speed or capacity. It is a change in how the project team looks at the process: the conveyor, filling head, container guidance, and downstream stations need to be considered as one operating sequence rather than as disconnected machines.
Continuous filling only works as part of a connected line
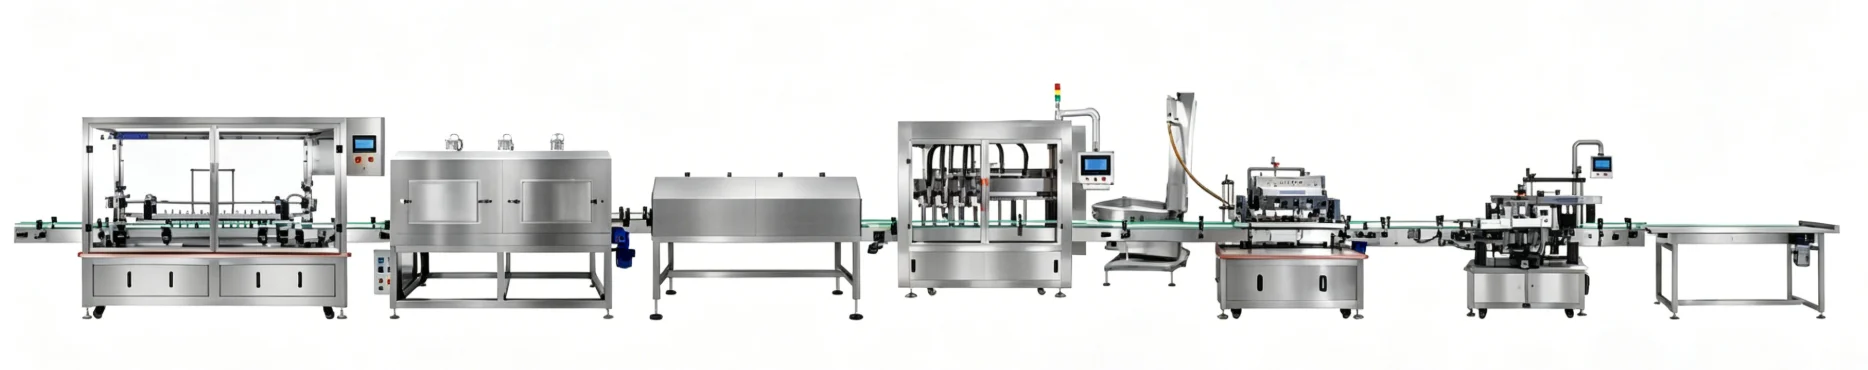
The documented BOJLINE process can be organized as bottle sorting, washing, drying, filling, capping, checkweighing, coding, labeling, sleeve shrinking, and collection. This sequence matters because the filler is not an isolated island: container preparation, filling, closure, inspection, identification, and collection all need a defined handoff.
For a factory evaluating a bottle or jar line, the practical question is therefore not simply “Can the filler fill?” It is “Can the complete line keep containers moving through the required operations, while providing the hygiene and traceability functions the product calls for?”
Hygiene, coding, and inspection are part of the rhythm
Tomato-food lines must also be evaluated beyond the filler. The available BOJLINE material identifies CIP in-place cleaning, steam vacuum capping, and food-grade design as relevant hygiene-oriented functions. These features address the way a food line is cleaned and closed; they do not replace confirmation of the specific hygiene requirements for a project.
At the downstream end, CO₂ laser coding can identify dates and batches, while metal detection and checkweighing can support quality checks and sorting. Together with capping and labeling, these functions turn continuous conveying into a controlled packaging sequence rather than simply a faster conveyor.
A better project discussion starts with the complete sequence
For a project manager or purchasing team, the first discussion should connect the product, container, line sequence, and integration boundary. Confirm whether the project needs bottle sorting, washing, drying, continuous filling, capping, checkweighing, coding, labeling, sleeve shrinking, collection, metal detection, or sorting and weighing. Then define which functions belong in the supplied line and which are handled by adjacent equipment.
The central value of the no-stop-bottle concept is process continuity. It gives the factory team a clearer basis for comparing a tomato sauce filling line: not an isolated filler with an assumed output, but a modular line whose filling, conveying, hygiene, identification, and inspection functions are discussed together and verified against the actual project.
Planning a tomato sauce packaging line?
Share your product, container, and line-integration requirements with the project team to discuss a suitable BOJLINE configuration without relying on unverified assumptions.